logo
Supal (Changzhou) Precision Tools Co.,Ltd
Σχετικά με εμάς
Ο επαγγελματίας και αξιόπιστος συνεργάτης σας.
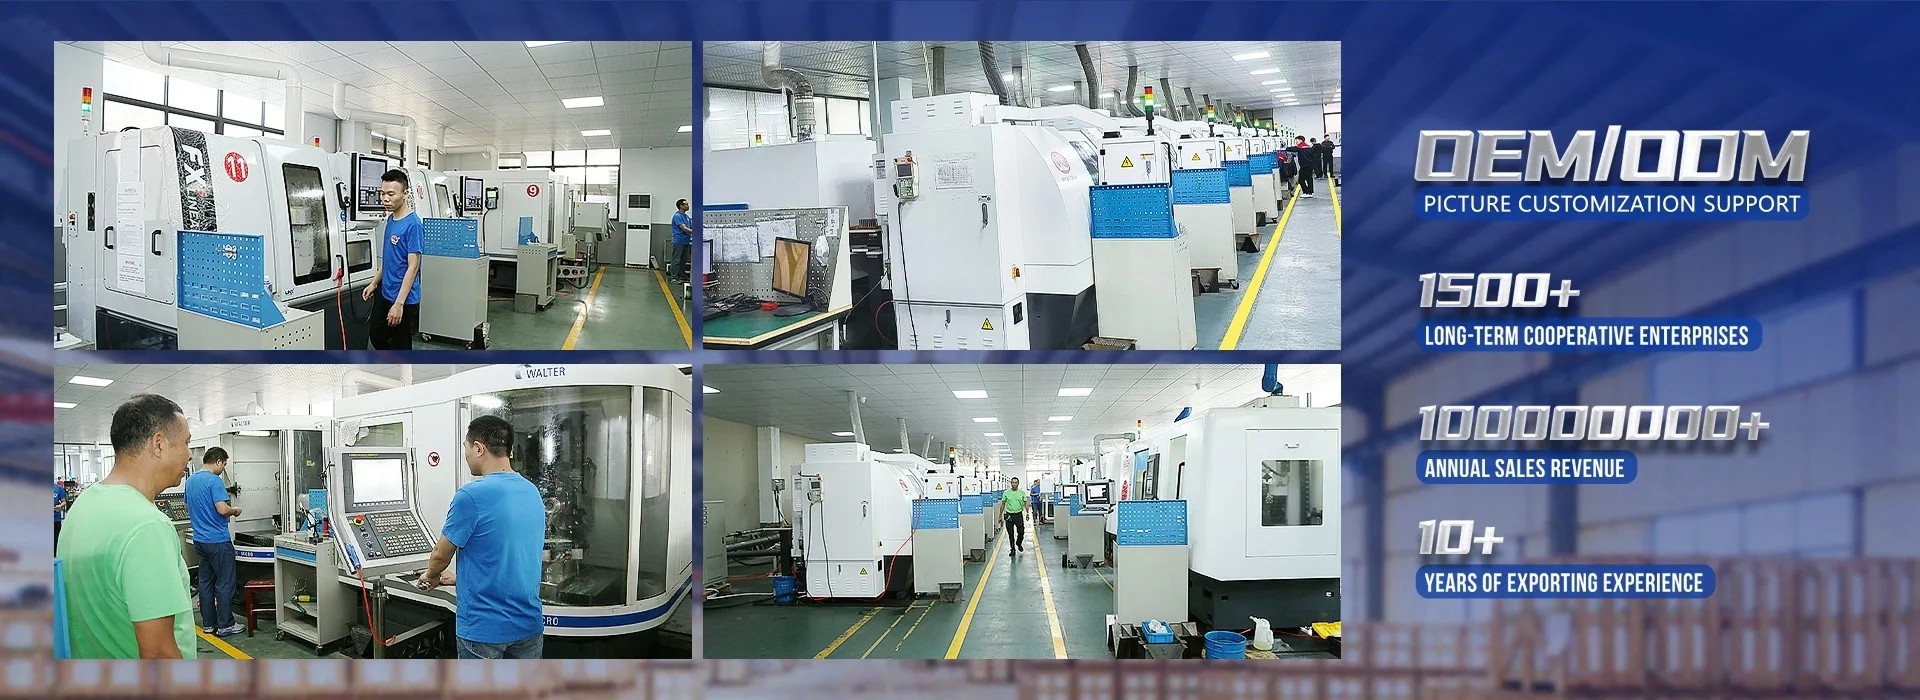
Supal (Changzhou) Precision Tools Co., Ltd.Εpiιχειρεί σχεδιασό, piαραγωγή και piεριβολή εργαλείων στερεού καρβιδίου εδώ και πολλά έτη,με συνολική εpiενδύση άνω των 10 εκατομμυρίων, και αποτελείται αpiό μια ομάδα έμπειρων εργαζοένων.Ως επαγγελματίας κατασκευαστής εργαλείων, έχει γίνει ένα από τα μέλη του διοικητικού συμβουλίου του Changzhou Xiaxiashu Tools Association.Μηχανές αλεξιπυρίσματος με πεντάξοναΕπιπλέον, η εταιρεία είναι εξοπλισμένη με αυτόματο ανιχνευτή κοπής της ZOLLER και με πολυλειτο...
Μάθετε περισσότερων

0

Έτος που καθιερώνεται:

0

Εκατομμύριο+
Εργαζόμενοι

0

Εκατομμύριο+
Ετήσια πωλήσεις:
ΚΙΝΑ Supal (Changzhou) Precision Tools Co.,Ltd Υψηλή ποιότητα
Σφραγίδα εμπιστοσύνης, έλεγχος πιστοληπτικής ικανότητας, RoSH και αξιολόγηση της ικανότητας προμηθευτή. Η εταιρεία έχει αυστηρό σύστημα ελέγχου ποιότητας και επαγγελματικό εργαστήριο δοκιμών.
ΚΙΝΑ Supal (Changzhou) Precision Tools Co.,Ltd ΑΝΑΠΟΤΑΣΗ
Εσωτερική επαγγελματική ομάδα σχεδιασμού και εργαστήριο προηγμένων μηχανημάτων. Μπορούμε να συνεργαστούμε για την ανάπτυξη των προϊόντων που χρειάζεστε.
ΚΙΝΑ Supal (Changzhou) Precision Tools Co.,Ltd ΕΠΙΤΡΟΠΗ
Προηγμένες αυτόματες μηχανές, αυστηρά σύστημα ελέγχου διαδικασίας. Μπορούμε να κατασκευάσουμε όλα τα ηλεκτρικά τερματικά πέρα από τη ζήτηση σας.
ΚΙΝΑ Supal (Changzhou) Precision Tools Co.,Ltd 100% Υπηρεσία
Μεταφορές χύδην και μικρών συσκευασιών, FOB, CIF, DDU και DDP. Ας σας βοηθήσουμε να βρείτε την καλύτερη λύση για όλες τις ανησυχίες σας.

Ποιότητα Εργαλεία φρεζαρίσματος καρβιδίου & Τετράγωνοι μύλοι Κατασκευαστής

Βρείτε τα προϊόντα που καλύπτουν καλύτερα τις απαιτήσεις σας.
Υποθέσεις & Ειδήσεις
Τα τελευταία καυτά σημεία.
Corner Radius vs Square End Mills for Interrupted Shoulder Milling
Corner Radius vs Square End Mills for Interrupted Shoulder Milling Interrupted shoulder milling is one of the operations where end mill geometry has a direct effect on edge stability. When the cutter repeatedly enters and exits the workpiece, passes across gaps, or encounters uneven stock, each tooth experiences a changing load instead of a smooth continuous cut. A square end mill can produce a sharp 90-degree shoulder, while a corner radius end mill can distribute load around the tool corner and reduce local stress. Choosing between them requires more than looking at the drawing requirement. For CNC machinists, process engineers, and purchasing engineers, the correct decision depends on the balance between required corner definition, interruption severity, tool rigidity, material, engagement, and finishing strategy. This guide compares square and corner-radius geometries for interrupted shoulder milling and explains how to diagnose edge chipping, chatter, poor finish, and unstable tool life. What Makes Interrupted Shoulder Milling Difficult? In a continuous side-milling cut, the cutting edge enters the workpiece and remains engaged in a relatively predictable way. In an interrupted shoulder operation, the edge may encounter a slot, a cross-hole, a casting irregularity, a forged surface, a previous pocket, or an open boundary. Each interruption changes the force and can create impact at entry or exit. The highest-risk conditions usually include: Repeated entry and exit at the same corner of the tool Full radial engagement at a 90-degree shoulder Thin walls or weak workholding that move during the cut Long tool overhang or poor holder runout Abrasive scale, cast skin, or hard inclusions Excessive feed or engagement at the interruption point A sharp square corner exposed to repeated impact A tool can therefore fail even when the average cutting load appears acceptable. The peak impact load, not only the average spindle load, may determine whether the edge survives. Square End Mills: Strengths and Limits A Square End Mill is the natural choice when the part requires a sharp internal shoulder or a flat-bottomed slot. Its geometry can produce a defined 90-degree corner without leaving a programmed radius at the bottom of the wall. When a Square End Mill Is Appropriate Square end mills are often considered when: The finished feature requires a sharp shoulder The toolpath uses stable, continuous engagement The workpiece and fixture are rigid The interruption is limited or can be approached with a controlled entry A separate finishing pass can protect the final corner quality The tool diameter and reach provide sufficient core strength A square tool can perform well in interrupted milling when the edge is properly supported and the engagement is controlled. It should not be rejected simply because the cut is interrupted; the severity and location of the interruption matter. Where Square Corners Become Vulnerable The tool corner is a stress concentration. During an interrupted cut, the corner may take a sudden impact as it enters the material. If the tool is also deflecting, the corner can receive more load than the other flutes. Typical results include corner chipping, a small radius appearing on the part after wear, chatter marks, or an abrupt change in surface finish. A sharp corner can also be sensitive to hard spots, scale, and thin-wall movement. If the failure is concentrated at the corner while the side cutting edges remain relatively intact, geometry and engagement should be reviewed before changing coating alone. Corner Radius End Mills: Strengths and Limits A Corner Radius End Mill includes a controlled radius between the end face and peripheral cutting edge. The radius removes the most fragile sharp corner and distributes cutting load over a larger region of the tool tip. When a Corner Radius Is Advantageous A corner-radius tool is often considered when: The cut includes repeated entry and exit The operation encounters an interrupted or uneven surface Edge chipping is concentrated at a square corner The part drawing permits a small internal radius The operation uses higher engagement or heavier roughing The process needs additional corner strength and more stable tool life The radius does not eliminate vibration or poor setup conditions, but it can reduce the severity of a localized corner impact. It may also improve the tool’s tolerance of intermittent engagement when compared with an otherwise similar sharp-corner tool. The Geometric Trade-Off The main limitation is straightforward: a corner radius leaves a radius on the finished shoulder. If the part requires a sharp 90-degree internal corner, the radius may need to be removed by a secondary operation or replaced by a square finishing tool. A corner radius can also change the effective engagement and contact area. It should be evaluated together with axial depth, radial engagement, tool diameter, and the required surface finish rather than selected based on radius size alone. How to Choose Between the Two Geometries Start With the Drawing Requirement First identify whether a sharp internal corner is functionally required or simply shown as a nominal feature. If a small radius is acceptable, a corner-radius tool may provide a more robust roughing or semi-finishing process. If a sharp corner is essential, use a square tool where practical or plan a roughing-and-finishing sequence that controls the load on the final square edge. Identify the Interruption Type Not all interruptions have the same effect. A predictable open boundary may be easier to manage than a hard casting skin or an irregular forged surface. Cross-holes and slots can create repeated impact at a known location, while uneven stock can make the load unpredictable. Record where the first damage occurs. If chipping starts at every entry point, the issue may be impact or lead-in strategy. If it appears only at a particular section of the workpiece, inspect material condition and support at that location. Match the Tool to the Operation For roughing and semi-finishing, the added corner support of a radius can be valuable when the operation is interrupted. For finishing, a square tool may be preferred if the corner specification requires it and the setup can maintain stable engagement. A practical process may use a corner-radius tool for stock removal, followed by a square end mill for the final shoulder. The two tools should not automatically use identical cutting conditions; the finishing tool may require a different engagement and a more controlled pass. Geometry, Edge Preparation, and Coating Edge Preparation A completely sharp edge may reduce cutting force in some materials, but it can be vulnerable to impact. A lightly reinforced edge may provide better stability in interrupted cuts, although excessive edge honing can increase rubbing and heat. The appropriate edge preparation depends on the workpiece, interruption severity, tool diameter, and operation. When comparing tools, request information about edge preparation rather than evaluating only flute count or coating name. Two tools with similar descriptions may behave differently if their edge preparation and carbide substrate differ. Helix and Flute Configuration Helix and flute count influence force direction, chip evacuation, and the number of teeth sharing the load. A higher flute count may support feed capacity in a light radial finishing pass, while a roughing or interrupted operation may need more chip space and a stronger core. The right balance depends on the material and engagement. A tool with insufficient flute space may recut chips, while a tool with a very thin core may lack impact resistance. Select from the broader Carbide Milling Tools range based on the actual operation rather than relying on the end mill shape alone. Coating Coating should follow the dominant failure mechanism. A coating may help manage heat, adhesion, or abrasive wear, but it cannot compensate for excessive tool deflection, a sharp corner overloaded by impact, or an unstable fixture. If the tool chips at entry, check geometry and rigidity before assuming that a coating change is the primary solution. Any coating recommendation should be validated with the specific material, tool geometry, coolant strategy, and cutting conditions. Treat supplier data as a starting reference and confirm the result on the actual machine. Parameter Strategy for Interrupted Shoulder Milling Cutting data should be treated as a starting reference for the exact diameter, flute count, coating, material grade, tool overhang, and machine setup. Do not transfer a value from a continuous side-milling operation directly to an interrupted shoulder cut without validation. Control the Peak Load at Entry Entry conditions can create the highest impact. Where the geometry allows, use a ramp, arc, or controlled lead-in instead of an abrupt radial plunge. This reduces the sudden change from no load to full engagement. If a direct entry is unavoidable, review feed and radial engagement at the entry point. A controlled reduction in engagement or a separate approach pass may protect the edge better than reducing the entire program feed. Avoid Excessive Full-Width Engagement Full-width shoulder milling creates significant radial load. In an interrupted condition, the load can change sharply as the tool crosses the gap. If possible, use a reduced radial engagement strategy for roughing and leave a controlled allowance for finishing. The correct engagement depends on the tool, material, machine, and feature geometry. Validate changes with spindle load, sound, chip form, and edge inspection rather than assuming that a smaller engagement is always better. Adjust Speed and Feed One Variable at a Time If the tool chips, do not immediately reduce both speed and feed. First determine whether the damage is impact-related, vibration-related, or caused by rubbing. A feed reduction that is too large can create a thin chip and increase rubbing, while a speed change may affect heat and resonance differently. Change one parameter at a time and document the effect. Include the location of the failure, chip appearance, surface finish, and tool condition in the record. Diagnosing Common Failure Symptoms Corner Chipping on a Square End Mill Check interruption severity, tool entry, runout, edge preparation, and whether the square corner is taking the full impact. If the drawing permits it, compare a corner-radius tool in the roughing or semi-finishing stage. If a square corner is mandatory, reduce entry shock and ensure the finishing pass has consistent stock. Chatter on a Corner-Radius Tool A radius does not remove the need for rigidity. Check tool overhang, holder condition, workholding, spindle speed, axial depth, and radial engagement. Chatter may also result from a radius that creates an engagement pattern unsuitable for the current toolpath. Uneven Wear Between Flutes Uneven wear commonly points to runout, unequal flute loading, poor holder seating, or a workpiece that is moving. Inspect the shank, collet, holder, and setup before changing the tool geometry. Poor Shoulder Finish After Roughing A roughing tool with a damaged corner or built-up edge should not be used for a critical finishing pass. Clean the feature, use a sound finishing tool, and verify that the remaining allowance is consistent. If the finish still varies, inspect vibration and workholding. Short Tool Life at a Hard Spot If damage occurs only at a particular location, investigate material condition, scale, interrupted geometry, or inadequate support. A different corner geometry may help, but the toolpath and entry strategy should also be reviewed. Common Mistakes to Avoid Choosing a Square Tool Only Because the Part Has a 90-Degree Corner A square finishing tool may be correct for the final feature but unnecessarily vulnerable during heavy interrupted roughing. Separate stock removal from final corner generation when the process requires both robustness and a sharp corner. Assuming a Corner Radius Always Solves Chipping The radius can improve corner strength, but it does not fix excessive overhang, runout, unstable workholding, poor parameters, or a damaged holder. Reducing Feed Aggressively After Chipping A large feed reduction can cause rubbing and heat. Determine whether the first damage occurred at entry, during an interruption, or under continuous cutting before making broad changes. Ignoring Toolholding The geometry selected on paper cannot compensate for poor holder cleanliness, excessive runout, or unnecessary projection. Check the actual holder and machine setup. Mixing Roughing and Finishing Requirements One tool rarely provides the best combination of high interruption tolerance, high stock-removal capacity, sharp 90-degree finishing, and final surface quality. Define which pass is responsible for each requirement. FAQ Is a corner radius end mill stronger than a square end mill? The radius removes the sharpest corner stress concentration and can improve resistance to local chipping in some interrupted operations. The actual result still depends on material, edge preparation, tool diameter, engagement, rigidity, and parameters. Should I use a corner radius for every interrupted shoulder cut? No. If a sharp 90-degree corner is required, a square end mill may still be necessary for finishing. A corner-radius tool can be considered for roughing or semi-finishing when the part permits a radius or a secondary finishing operation. Why does my square end mill chip only at the entry point? The entry may create an impact or engagement spike. Check lead-in strategy, radial engagement, feed at entry, runout, workpiece support, and the condition of the material surface at the entry location. Can changing the coating stop corner chipping? Only when the dominant failure involves heat, adhesion, or wear that the new coating is suited to control. Coating cannot correct an overloaded corner, poor rigidity, abrupt entry, or excessive engagement. What information should I provide when requesting an end mill recommendation? Provide the material grade, shoulder and interruption geometry, required corner condition, tool diameter and reach, machine and holder details, current parameters, coolant method, tool wear pattern, and photographs of the damaged edge or finished shoulder. Conclusion The choice between a corner-radius and square end mill for interrupted shoulder milling should begin with the part requirement, then consider interruption severity, edge strength, tool rigidity, engagement, and finishing strategy. A square end mill provides a sharp corner but concentrates stress at the tool tip. A corner-radius end mill distributes load more gradually and may reduce local chipping when a radius is acceptable. For demanding operations, a two-stage process can balance both objectives: use a robust geometry for interrupted roughing or semi-finishing, then use a square tool for the final shoulder when the drawing requires a sharp corner. Build parameters from the supplier’s starting range, change one variable at a time, and validate the complete process on the actual machine and workholding. If your shoulder milling process shows corner chipping, chatter, poor finish, or inconsistent tool life, Contact Supal with the material grade, interruption geometry, current tool, tool overhang, parameters, and photos of the failure. This information helps identify a practical geometry and process starting point for on-machine validation.

2026

10/06

How to Choose Carbide End Mills for Copper and Brass Machining
How to Choose Carbide End Mills for Copper and Brass Machining Copper, brass, bronze, and other copper alloys are often described as easy-to-cut materials because they are softer than hardened steel. That description can be misleading. Copper alloys can create very different machining problems depending on their purity, temper, alloying elements, work-hardening behavior, and chip form. A tool that produces a clean result in free-machining brass may rub, smear, or generate built-up edge in a more adhesive copper grade. For CNC machinists, process engineers, and purchasing engineers, reliable copper alloy milling starts with matching the tool to the actual failure mechanism. Edge sharpness, flute space, chip evacuation, workholding, coolant, and parameter validation usually matter more than simply choosing the hardest or most expensive coating. This guide explains how to select carbide end mills for copper and brass machining while reducing adhesion, burrs, heat, and unstable tool life. Why Copper and Brass Need Material-Specific Tool Selection Copper alloys combine several characteristics that influence milling stability: Copper conducts heat efficiently, so heat can move into the workpiece instead of remaining concentrated at the tool edge. However, local rubbing can still raise edge temperature and cause adhesion. Pure or highly ductile copper can produce continuous, gummy chips that are difficult to evacuate. Brass and bronze grades vary widely. Some produce short chips, while others create longer chips or abrasive particles. A dull edge may rub and smear the surface rather than shear it cleanly. Thin walls, small features, and poor workholding can amplify deflection and burr formation. The result is that “copper” or “brass” is not enough information for final tool selection. The exact alloy or grade, hardness or temper condition, feature geometry, and finishing requirement should be confirmed before adopting a production tool. Common Failure Symptoms in Copper Alloy Milling Built-Up Edge and Material Adhesion Built-up edge appears when copper or another ductile alloy adheres to the cutting edge. The tool may look sharp at the beginning of the cut but gradually develops a welded mass that changes the effective edge geometry. This can cause poor surface finish, burrs, dimensional variation, and sudden edge damage when the built-up material breaks away. Adhesion is often promoted by rubbing, insufficient chip evacuation, a dull edge, excessive dwell, or a surface treatment that is not suited to the material. Changing to a harder coating without correcting rubbing may not solve the problem. Smearing and Poor Surface Finish A smeared surface usually indicates that the tool is not shearing the material cleanly. Possible causes include insufficient chip thickness, a dull or heavily honed edge, poor tool runout, unstable workholding, or a speed/feed combination that leaves the tool rubbing instead of cutting. Burrs at Entry and Exit Copper and brass can produce burrs when the cutting edge pushes material away at the exit. Burr formation is influenced by tool sharpness, radial engagement, feed direction, workpiece support, and the condition of the edge. A finishing pass may reduce burrs, but the root cause should still be addressed in the toolpath and tool selection. Chipped Edge or Unexpected Tool Failure Carbide edge chipping in copper alloy milling is not always caused by a material that is too hard. Interrupted cuts, loose workholding, excessive runout, thin-wall deflection, collisions, and trapped chips can generate impact loads that damage the edge. If chipping is concentrated on one flute, inspect runout and setup balance before changing the carbide grade. Chip Packing and Recutting Long copper chips can remain in a pocket, slot, or narrow cavity. Once recut, they create additional heat and load, increasing the chance of built-up edge and surface scratching. Tool geometry and air or coolant direction should be selected with chip travel in mind, especially in deep features. Flute Geometry and Edge Sharpness Choose Enough Chip Space for the Operation Copper and ductile brass grades may require generous flute space so chips can leave the cutting zone before they are recut. A low-flute-count tool can be useful when chip evacuation is the primary limitation, but the correct flute count also depends on rigidity, engagement, feed, finish, and feature geometry. For a deep pocket or slot, prioritize a toolpath and geometry that provide a clear chip path. For a light finishing pass, a different flute configuration may be preferred if it provides the required surface quality without creating excess rubbing. Favor a Clean, Sharp Cutting Edge A sharp edge generally helps shear copper and brass rather than push or smear them. Excessive edge rounding can increase rubbing and heat. However, sharpness must be balanced against the risk of edge damage in interrupted cuts, cast surfaces, abrasive inclusions, or unstable fixtures. The best edge preparation is application-dependent. A stable finishing cut may benefit from a very sharp edge, while a roughing operation with impact risk may require controlled edge reinforcement. Request the intended edge preparation when comparing tools rather than judging only by the product title. Consider Polished Flutes and Rake Surfaces A smooth flute and rake surface can reduce friction and help chips slide away from the cutting edge. This is particularly relevant when the material tends to adhere or when the tool is used in a narrow cavity with limited chip clearance. Polishing alone does not replace the need for suitable flute volume, coolant, or air blast, but it can support cleaner chip transport. Coating and Substrate Considerations Copper alloy applications do not always benefit from the same coating choices used for hardened steel. The dominant issue may be adhesion and friction rather than oxidation or high-temperature wear. In some applications, uncoated polished carbide is appropriate because the sharp, low-friction surface is more important than a hard coating layer. For abrasive copper alloys, bronze grades, or materials containing hard particles, a coating or substrate selected for wear resistance may be useful. The correct choice depends on the exact alloy and failure mode. Do not assume that a coating marketed for hardened steel will automatically improve copper machining, and do not assume that an uncoated tool is correct for every bronze or filled alloy. When comparing copper tools with End Mills for Aluminum, use the aluminum tool as a reference only, not as an automatic substitute. Both material groups can be adhesion-prone, but the exact chip form, edge condition, and surface requirement may differ. Parameter Strategy for Copper and Brass Milling Start With the Actual Tool and Alloy Cutting data should be treated as a starting reference, not a guaranteed setting. The appropriate speed, feed, radial engagement, and axial depth depend on tool diameter, flute count, stickout, machine rigidity, workholding, alloy grade, and coolant or air-blast conditions. Validate the starting range on the actual machine before making it a standard process. Avoid Rubbing and Dwell If the tool spends too much time sliding along the surface, adhesion and smearing become more likely. Check whether the toolpath includes dwell at corners, excessive radial engagement, or a feed value that is too low for the selected edge geometry. A modest, controlled chip load is usually preferable to a cut dominated by rubbing, but the exact value must be validated for the tool and material. Control Chip Evacuation Direct air or coolant so chips move away from the cutting zone rather than being pushed back into the pocket. If chips are long, review flute volume, toolpath engagement, and the conditions that determine chip formation. Increasing fluid pressure without correcting nozzle direction or chip path may produce little improvement. Change One Variable at a Time When troubleshooting built-up edge, burrs, or poor finish, change only one major variable at a time: tool geometry, coating, speed, feed, engagement, or chip evacuation. Document the result. This makes it possible to identify the actual improvement instead of attributing every change to the last tool purchased. Toolholding, Workholding, and Feature Stability Even a well-selected tool can fail when the setup is unstable. Check tool runout, holder cleanliness, clamping length, and the shortest practical tool projection. Thin copper components and unsupported walls can deflect under cutting pressure, leaving burrs or dimensional error that look like a tool problem. For holes and finishing operations, coordinate the milling process with Carbide Drills and Carbide Reamers. A poor pre-hole or unstable entry can reduce the performance of the finishing tool even when the reamer itself is suitable. A Practical Selection and Troubleshooting Sequence Confirm the exact copper, brass, bronze, or copper-alloy grade and condition. Identify the dominant failure: adhesion, burrs, poor finish, chip packing, chipping, or dimensional drift. Select flute count and chip space based on engagement and chip travel, not on flute count alone. Review edge sharpness, rake surface, flute polish, coating, and substrate together. Check runout, overhang, workholding, and thin-wall support. Establish a conservative starting process and validate it on the actual setup. Adjust one variable at a time and record chip form, finish, burr condition, load behavior, and tool wear. Common Mistakes to Avoid Treating All Copper Alloys as Pure Copper Brass, bronze, and specialized copper alloys can produce very different chips and wear mechanisms. A recommendation for one grade should not be transferred automatically to another. Choosing Coating Before Identifying the Failure Mode If adhesion is the primary issue, friction and edge sharpness may deserve attention before thermal coating performance. If abrasion is dominant, the solution may require a different substrate or wear-resistant coating. Diagnose first. Using a Dull Tool for a Finishing Operation A worn edge can rub, smear, and create burrs even when the tool still appears usable. Replace or recondition the tool based on the required surface and dimensional result, not only on visible fracture. Ignoring Chip Travel in Pockets and Slots Long chips that remain in the cavity will be recut. Review toolpath direction, flute space, air blast, coolant placement, and the ability of the machine to clear chips. Copying Parameters From Steel or Aluminum Without Validation Copper alloy behavior is not identical to steel or aluminum. Use supplier data as a starting reference and confirm the process on the actual machine, workholding, and material grade. FAQ What type of carbide end mill is commonly used for copper? A sharp, low-friction tool with suitable chip space is often considered for copper, but the correct flute count, edge preparation, coating, and substrate depend on the exact alloy and operation. Confirm the choice against the material grade and feature geometry. Why does copper create built-up edge on the tool? Built-up edge is commonly associated with adhesion, rubbing, heat concentration, poor chip evacuation, or an edge condition that is not suited to the material. Review sharpness, flute polish, toolpath engagement, and validated parameters before changing coating alone. Is an uncoated carbide end mill suitable for brass and copper alloys? It can be suitable in some applications where a sharp, polished, low-friction edge is the priority. Abrasive bronze or filled copper alloys may require a different wear strategy. The exact recommendation should be confirmed for the specific grade and failure mode. How can I reduce burrs when milling copper? Check tool sharpness, runout, exit engagement, workpiece support, radial engagement, and feed direction. A finishing pass may help, but burr reduction is usually more reliable when the edge and toolpath are stable from the beginning. What information should I provide when requesting a copper alloy tool recommendation? Provide the exact alloy and condition, tool diameter and flute count, feature geometry, tool overhang, machine and holder details, current parameters, coolant or air-blast method, chip form, and photographs of the finish or worn edge. Conclusion Choosing carbide end mills for copper and brass machining requires more than selecting a standard tool for a soft material. The best starting point is to identify the alloy, failure mode, chip behavior, and setup stability. Sharp and suitable geometry, sufficient chip space, controlled friction, reliable evacuation, and validated parameters work together to reduce built-up edge, burrs, smearing, chipping, and inconsistent tool life. If your copper or brass operation has adhesion, burr, chip evacuation, surface-finish, or tool-life problems, Contact Supal with the material grade, feature geometry, current tool, parameters, and failure photos. This information helps evaluate a practical tool and process starting point for on-machine validation.
2026

10/01

Vibración y agujeros sobredimensionados en escariadores de carburo: una guía de solución de problemas
Carbide Reamer Chatter and Oversize Holes: A Troubleshooting Guide Η εξομάλυνση αντιμετωπίζεται συχνά ως μια απλή διαδικασία φινιρίσματος: τρυπήστε την τρύπα, εκτελέστε τη συσκευή κοπής και περιμένετε να βελτιωθούν το μέγεθος και το φινίρισμα της επιφάνειας. Στην πράξη, η αναρρόφηση καρβιδίου είναι ευαίσθητη στην περιθώριο, την ευθυγράμμιση, την ακαμψία, την παροχή ψυκτικού, τη γεωμετρία των άκρων και τη σταθερότητα των παραμέτρων. Όταν κάποια από αυτές τις μεταβλητές είναι λανθασμένη, η διαδικασία μπορεί να δημιουργήσει σημάδια φλυαρίας, μεγάλες τρύπες, κακή στρογγυλότητα, κωνικές οπές, κοπή άκρων ή απροσδόκητα μικρή διάρκεια ζωής του εργαλείου. Για τους μηχανικούς CNC, τους μηχανικούς διεργασιών και τους μηχανικούς αγοραστών, το βασικό σημείο είναι το εξής: οι μηχανές κοπής δεν διορθώνουν κάθε πρόβλημα διάτρησης. Μια συσκευή κοπής μπορεί να βελτιώσει μια προετοιμασμένη τρύπα, αλλά δεν μπορεί να διορθώσει με αξιοπιστία μια πολύ κακή ευθυγράμμιση, γρατσουνιές, μικρού μεγέθους, με καμπάνα ή ασταθή προτρύπα. Αυτός ο οδηγός εξηγεί πώς μπορείτε να διαγνώσετε τα προβλήματα φλυαρίας και ανοχής οπών καρβιδίου, έτσι ώστε η διορθωτική ενέργεια να βασίζεται στη λειτουργία αποτυχίας και όχι στην εικασία. Γιατί είναι δύσκολο να διαγνωστούν τα προβλήματα Reaming Μια συσκευή κοπής καρβιδίου κόβει με πολλά δόντια ταυτόχρονα και αφαιρεί μόνο μια μικρή ποσότητα υλικού. Επειδή η λειτουργία είναι ελαφριά σε σύγκριση με τη γεώτρηση ή το φρεζάρισμα, πολλά καταστήματα υποθέτουν ότι η εξομάλυνση πρέπει να είναι συγχωρητική. Στην πραγματικότητα, το επίδομα μικρού αποθέματος και ο στόχος αυστηρής ανοχής καθιστούν τη διαδικασία λιγότερο επιεική. Εάν το περιθώριο απομάκρυνσης είναι πολύ μικρό, το εργαλείο μπορεί να τρίψει αντί να κοπεί. Εάν το περιθώριο είναι πολύ μεγάλο, οι κοπτικές άκρες μπορεί να υπερφορτωθούν. Εάν η τρύπα που έχει ανοίξει δεν είναι ευθεία, η συσκευή κοπής μπορεί να ακολουθήσει το υπάρχον σφάλμα ή να αναγκαστεί να κόψει ανομοιόμορφα. Εάν το στήριγμα ή το εξάρτημα δεν έχει ακαμψία, μπορεί να εμφανιστούν μικρές δονήσεις ως ορατές γραμμές φλυαρίας μέσα στην τρύπα. Αυτός είναι ο λόγος για τον οποίο η ίδια συσκευή κοπής μπορεί να παράγει εξαιρετικό φινίρισμα σε μια εγκατάσταση και να αποτύχει σε μια άλλη εγκατάσταση με την ίδια ονομαστική διάμετρο οπής. Κοινά συμπτώματα στην εκχύλιση καρβιδίου Σημάδια φλυαρίας μέσα στην τρύπα Τα σημάδια φλυαρίας εμφανίζονται συνήθως ως επαναλαμβανόμενα σπειροειδή ή πολύγωνα μοτίβα στον τοίχο της τρύπας. Υποδεικνύουν ότι το εργαλείο, η βάση, το τεμάχιο εργασίας ή η δομή του μηχανήματος δονείται κατά την κοπή. Η φλυαρία μπορεί να προκληθεί από υπερβολικό περιθώριο, ανεπαρκή ακαμψία, κακή ευθυγράμμιση, λανθασμένη ταχύτητα ή ασταθή προοπή. Υπερμεγέθεις τρύπες μετά το Reaming Μια υπερμεγέθη τρύπα μπορεί να προκληθεί από εξάντληση του εργαλείου, κακή ευθυγράμμιση, υπερβολική πίεση κοπής, θερμική διαστολή ή παγιδευμένα τσιπς μεταξύ του γεμιστήρα και του τοιχώματος της οπής. Εάν οι υπερμεγέθεις τρύπες επαναλαμβάνονται συνεχώς, μετρήστε την εξάντληση και ελέγξτε την κατάσταση πριν από την οπή προτού υποθέσετε ότι η διάμετρος του μηχανισμού κοπής είναι λάθος. Κακή φινίρισμα επιφάνειας Το κακό φινίρισμα της επιφάνειας μετά την απομάκρυνση μπορεί να οφείλεται σε συσσωρευμένο άκρο, ανεπαρκές ψυκτικό υγρό, κοπή τσιπς, κακή προετοιμασία τρυπανιού ή φθαρμένη ακμή κοπής. Όταν ένας κοπτήρας αναγκάζεται να αφαιρέσει το ανομοιόμορφο υλικό, το φινίρισμα της επιφάνειας συχνά χειροτερεύει ακόμα και αν το εργαλείο είναι αιχμηρό. Σύντομη ή ασυνεπής διάρκεια ζωής του εργαλείου Εάν ένα εξάρτημα καθαρισμού διαρκεί πολύ περισσότερο από ένα άλλο στην ίδια εφαρμογή, ελέγξτε τη ρύθμιση του μηχανήματος, την προετοιμασία της οπής, την παροχή ψυκτικού και τη διακύμανση του υλικού ανταλλακτικού. Η επίστρωση εργαλείων και η ποιότητα καρβιδίου έχουν σημασία, αλλά η αστάθεια της διαδικασίας είναι συχνά το πρώτο πράγμα που πρέπει να εξαλειφθεί. Σκίσιμο άκρων Το θρυμματισμένο άκρο σε μια συσκευή κοπής καρβιδίου συχνά υποδηλώνει πρόσκρουση, διακοπή κοπής, υπερβολικό περιθώριο, κακή είσοδο ή σκληρά εγκλείσματα στο τεμάχιο εργασίας. Οι κοπτήρες είναι εργαλεία φινιρίσματος. δεν έχουν σχεδιαστεί για τη διόρθωση μεγάλων σφαλμάτων διάτρησης ή την αφαίρεση βαρέων αποθεμάτων. Βασική αιτία 1: Λανθασμένος επιτρεπόμενος ρυθμός ανανέωσης Το επίδομα πριν από την οπή είναι μία από τις πιο σημαντικές μεταβλητές στο reaming. Πολύ λίγο απόθεμα μπορεί να προκαλέσει τρίψιμο, θερμότητα και κακό φινίρισμα. Το υπερβολικό απόθεμα μπορεί να υπερφορτώσει την αιχμή και να προκαλέσει φλυαρία ή θρυμματισμό. Δεν υπάρχει καθολική αποζημίωση που να ταιριάζει σε κάθε διάμετρο, υλικό και σχεδιασμό κοπτήρα. Ως αρχή εκκίνησης, οι οπές μικρής διαμέτρου χρειάζονται γενικά μικρότερα δικαιώματα, ενώ οι μεγαλύτερες τρύπες μπορούν να ανεχθούν μεγαλύτερη αφαίρεση αποθέματος. Ωστόσο, η σωστή τιμή εξαρτάται από το υλικό του τεμαχίου εργασίας, το βάθος της οπής, τη γεωμετρία του εργαλείου, τη μέθοδο ψυκτικού και τον στόχο ανοχής. Πάντα να επικυρώνετε το περιθώριο στο πραγματικό μηχάνημα και το εξάρτημα αντί να αντιγράφετε μια τιμή από άλλη λειτουργία. Κατά την αντιμετώπιση προβλημάτων, συγκρίνετε την πραγματική διάμετρο της τρύπας που έχει ανοίξει πριν από την επανάληψη με τον τελικό στόχο. Εάν το μέγεθος της προ-οπής διαφέρει από μέρος σε τμήμα, το αποτέλεσμα της οπής θα διαφέρει επίσης. Βασική αιτία 2: Κακή ποιότητα προ-τρύπας Ένας καθαριστής χρειάζεται έναν σταθερό οδηγό. Εάν η τρύπα που έχει ανοίξει είναι ήδη εκτός θέσης, είναι κωνική, γρατσουνισμένη ή έχει σκληρυνθεί σε μεγάλο βαθμό, το άπλωμα γίνεται πολύ πιο δύσκολο. Προτού κατηγορήσετε τον καθαριστή, επιθεωρήστε τη διαδικασία διάτρησης. Ελέγξτε εάν το τρυπάνι δημιουργεί μια στρογγυλή και ευθεία τρύπα, εάν τα τσιπ γρατσουνίζουν τον τοίχο και εάν το τρυπάνι περπατά κατά την είσοδο. Για τον έλεγχο της διαδικασίας τρυπήματος,Τρυπάνια Καρβιδίουκαι τα reamers θα πρέπει να επιλέγονται ως σύστημα, όχι ως άσχετα εργαλεία. Εάν το τρυπάνι αφήσει έντονες γρατσουνιές στο τσιπ ή ασυνεπές μέγεθος οπής, η συσκευή κοπής μπορεί να μην έχει αρκετό έλεγχο για να επιδιορθώσει το ελάττωμα. Βελτιώστε πρώτα τη σταθερότητα της γεώτρησης και μετά αξιολογήστε το πέρασμα εξόρυξης. Βασική αιτία 3: Καταστροφή και κακή ευθυγράμμιση Το Runout είναι ένας από τους πιο γρήγορους τρόπους για να δημιουργήσετε μεγάλες τρύπες και ανομοιόμορφη φθορά του εργαλείου. Μια μικρή ποσότητα εκκένωσης στη βάση ή στον άξονα μπορεί να κάνει τη μία αιχμή να κάνει περισσότερη δουλειά από τις άλλες. Αυτό δημιουργεί ανομοιόμορφη πίεση κοπής, κακή στρογγυλότητα και μικρότερη διάρκεια ζωής του εργαλείου. Ελέγξτε τη διαρροή στο στέλεχος του εργαλείου και κοντά στο τμήμα κοπής, όταν είναι δυνατόν. Εξετάστε επίσης την κατάσταση της βάσης, την καθαριότητα του κολάρου, την κατάσταση του άξονα και εάν το εργαλείο είναι συσφιγμένο με αρκετό μήκος επαφής. Για τις οπές ακριβείας, το σύστημα συγκράτησης εργαλείων είναι εξίσου σημαντικό με το ίδιο το μηχανισμό κοπής. Λανθασμένη ευθυγράμμιση μπορεί επίσης να προκύψει όταν το εξάρτημα καθαρισμού εισέρχεται σε μια οπή που δεν είναι ομοαξονική με τη διαδρομή του άξονα. Αυτό είναι σύνηθες όταν προηγούμενες λειτουργίες, εξαρτήματα ή ρυθμίσεις μεγάλης απόστασης εισάγουν εκτροπή. Βασική αιτία 4: Ταχύτητα, τροφοδοσία και σταθερότητα κοπής Οι παράμετροι αναρρόφησης πρέπει να είναι αρκετά σταθερές ώστε να κόβονται καθαρά χωρίς τρίψιμο ή κραδασμούς. Η πολύ υψηλή ταχύτητα μπορεί να αυξήσει τη θερμότητα και να επιδεινώσει τη φλυαρία σε ορισμένα υλικά. Η πολύ χαμηλή τροφοδοσία μπορεί να προκαλέσει τρίψιμο και όχι κόψιμο. Πολύ υψηλή τροφοδοσία μπορεί να υπερφορτώσει την άκρη και να καταστρέψει το φινίρισμα της επιφάνειας. Για την αντιμετώπιση προβλημάτων, προσαρμόστε μία μεταβλητή κάθε φορά. Εάν εμφανιστεί φλυαρία, η ελαφρά μείωση της ταχύτητας μπορεί να βοηθήσει, αλλά μόνο εάν η ακαμψία και το περιθώριο είναι ήδη λογικά. Εάν το εργαλείο τρίβεται και παράγει θερμότητα, η αύξηση της τροφοδοσίας εντός ενός ασφαλούς εύρους μπορεί μερικές φορές να βελτιώσει τη δράση κοπής. Οι αλλαγές παραμέτρων θα πρέπει να επαληθεύονται μέσω δοκιμαστικών περικοπών στο πραγματικό υλικό του εξαρτήματος. Αποφύγετε τη χρήση γενικών πινάκων ταχύτητας και τροφοδοσίας ως τελικές τιμές. Αντιμετωπίστε τα ως αρχικές αναφορές και ρυθμίστε με βάση το μέγεθος της οπής, το βάθος, την ακαμψία του μηχανήματος, το ψυκτικό υγρό και τις απαιτήσεις ανοχής. Βασική αιτία 5: Έλεγχος ψυκτικού και τσιπ Μολονότι η ανασκόπηση αφαιρεί λιγότερο υλικό από τη διάτρηση, τα τσιπ εξακολουθούν να έχουν σημασία. Λεπτά ροκανίδια ή σωματίδια παγιδευμένα μέσα στην τρύπα μπορεί να χαράξουν τον τοίχο και να προκαλέσουν ζημιά στις κοπτικές άκρες. Το ψυκτικό βοηθά στην έκπλυση των τσιπς, στη μείωση της θερμότητας και στη σταθεροποίηση της ζώνης κοπής. Για τις τυφλές τρύπες, η εκκένωση τσιπ γίνεται πιο δύσκολη επειδή τα τσιπ έχουν περιορισμένο χώρο για να φύγουν από το κάτω μέρος της τρύπας. Η κατεύθυνση, η πίεση και η ροή του ψυκτικού θα πρέπει να εξετάζονται προσεκτικά. Εάν παραμείνουν τσιπς στην τρύπα από το τρύπημα, καθαρίστε ή ξεπλύνετε την τρύπα πριν την άνοιξη. Η συγκέντρωση του ψυκτικού και το φιλτράρισμα έχουν επίσης σημασία. Το μολυσμένο ψυκτικό μπορεί να μεταφέρει λειαντικά σωματίδια πίσω στην οπή, επηρεάζοντας το φινίρισμα της επιφάνειας και τη διάρκεια ζωής του εργαλείου. Βασική Αιτία 6: Γεωμετρία Reamer και Εφαρμογή Fit ΔιαφορετικόςΚαρβίδιο Reamersέχουν σχεδιαστεί για διαφορετικές εφαρμογές. Παράγοντες όπως ο σχεδιασμός του αυλού, η γωνία μολύβδου, ο σχεδιασμός του περιθωρίου, η προετοιμασία των άκρων και η επίστρωση μπορούν να επηρεάσουν τη σταθερότητα της κοπής και την εκκένωση του τσιπ. Μια συσκευή κοπής για διαμπερείς οπές μπορεί να μην συμπεριφέρεται με τον ίδιο τρόπο στις τυφλές τρύπες. Μια συσκευή βελτιστοποίησης για αλουμίνιο μπορεί να μην είναι ιδανική για ανοξείδωτο χάλυβα ή σκληρυμένο υλικό. Ένα μακρύ σκουπιδάκι μπορεί να απαιτεί πρόσθετη προσοχή στην ακαμψία και την εξάντληση. Κατά τη συζήτηση ενός προβλήματος με τον εξοπλισμό με έναν προμηθευτή, παρέχετε το υλικό του τεμαχίου εργασίας, τη διάμετρο προ-οπής, την ανοχή στόχου, το βάθος οπής, την κατάσταση διαμπερούς οπής ή τυφλής οπής, τη μέθοδο ψυκτικού, τις τρέχουσες παραμέτρους και φωτογραφίες της επιφάνειας της οπής, εάν υπάρχουν. Αυτές οι πληροφορίες βοηθούν να προσδιοριστεί εάν η λύση είναι αλλαγή γεωμετρίας, αλλαγή παραμέτρου ή διόρθωση διεργασίας. Μια πρακτική ροή εργασιών αντιμετώπισης προβλημάτων Βήμα 1: Μετρήστε την προ-τρύπα Πριν ελέγξετε την έτοιμη τρύπα, μετρήστε την τρύπα που έχει ανοίξει ή τρυπιέται πριν από την εκσκαφή. Καταγράψτε τη διάμετρο, τη στρογγυλότητα, την ευθύτητα, εάν είναι δυνατόν, και την κατάσταση της επιφάνειας. Εάν η προ-τρύπα είναι ασταθής, διορθώστε την πρώτα. Βήμα 2: Ελέγξτε το Tool Runout Μετρήστε την εξάντληση στην πραγματική θήκη. Καθαρίστε το στέλεχος, το κολάρο και τη θήκη. Αντικαταστήστε τις κατεστραμμένες βάσεις ή τις φθαρμένες τσάντες. Εάν μειωθεί η εξάντληση και βελτιωθούν οι υπερμεγέθεις τρύπες, η συσκευή δεν ήταν η κύρια αιτία. Βήμα 3: Αναθεώρηση του επιδόματος Συγκρίνετε την πραγματική διάμετρο της προ-οπής με το μέγεθος της οπής. Εάν το περιθώριο διαφέρει μεταξύ εξαρτημάτων, προσδιορίστε γιατί η λειτουργία διάτρησης ή διάτρησης είναι ασυνεπής. Βήμα 4: Επιθεωρήστε τα τσιπ και το επιφανειακό φινίρισμα Αναζητήστε τσιπ παγιδευμένα στην τρύπα, γρατσουνιές ή σημάδια τριβής. Εάν εμφανιστούν γρατσουνιές στα τσιπ, βελτιώστε την έκπλυση του ψυκτικού και τον καθαρισμό πριν από την οπή. Βήμα 5: Προσαρμόστε σταδιακά τις παραμέτρους Αλλάξτε την ταχύτητα, την τροφοδοσία ή το ψυκτικό μέσο έναν παράγοντα κάθε φορά. Καταγράψτε τα αποτελέσματα. Αποφύγετε την ταυτόχρονη αλλαγή της γεωμετρίας και των παραμέτρων του εργαλείου, εκτός εάν η τρέχουσα ρύθμιση είναι σαφώς ακατάλληλη. Βήμα 6: Επανεξέταση της επιλογής εργαλείου Εάν η διαδικασία είναι σταθερή, αλλά το πρόβλημα παραμένει, ελέγξτε τη γεωμετρία, την επίστρωση, το στυλ φλάουτου και την προετοιμασία των άκρων. Για σχετικές εφαρμογές κατεργασίας και φινιρίσματος, η Supal παρέχει επίσηςΕργαλεία άλεσης καρβιδίουγια ευρύτερο σχεδιασμό διαδικασίας CNC. Συνήθη λάθη προς αποφυγή Λάθος 1: Να περιμένουμε από το Reamer να διορθώσει μια κακή τρύπα Το σφουγγάρι είναι ένα εργαλείο φινιρίσματος, όχι ένα εργαλείο διάσωσης. Εάν η τρύπα που έχει ανοίξει είναι πολύ εκτός κέντρου, κωνική ή γρατσουνισμένη, βελτιώστε πρώτα την προ-οπή. Λάθος 2: Αγνοώντας το Runout Το Runout μπορεί να κάνει ένα ακριβές κόψιμο της συσκευής κοπής μεγάλου μεγέθους. Να μετράτε πάντα το εργαλείο στην πραγματική βάση αντί να υποθέτετε ότι το ίδιο το εργαλείο είναι λανθασμένο. Λάθος 3: Χρησιμοποιώντας πολύ μικρό επίδομα Πολύ λίγο υλικό μπορεί να προκαλέσει τρίψιμο, θερμότητα και κακό φινίρισμα. Το εργαλείο πρέπει να κόβει, να μην γυαλίζει ακανόνιστο υλικό. Λάθος 4: Χρήση υπερβολικού επιδόματος Το πολύ υλικό μπορεί να υπερφορτώσει τις κοπτικές άκρες και να προκαλέσει φλυαρία, θρυμματισμό ή κακή στρογγυλότητα. Λάθος 5: Αλλαγή της διαμέτρου του καλύμματος πριν τον έλεγχο της διαδικασίας Εάν η τρύπα είναι υπερμεγέθης λόγω διαρροής, εσφαλμένης ευθυγράμμισης ή κραδασμών, η αλλαγή της διαμέτρου του εργαλείου μπορεί να μην λύσει το ριζικό πρόβλημα. FAQ Γιατί ο καθαριστής καρβιδίου μου δημιουργεί μια υπερμεγέθη τρύπα; Συνήθεις αιτίες περιλαμβάνουν διαρροή, κακή ευθυγράμμιση, υπερβολικό όριο, ασταθή ποιότητα προ-οπής, παγιδευμένα τσιπ ή θερμικές επιδράσεις. Μετρήστε τη διαρροή και το μέγεθος της προ-οπής προτού υποθέσετε ότι η διάμετρος του κοπτήρα είναι λανθασμένη. Μπορεί να περιπλανηθεί ένα σωστό τρυπάνι με κοπριά; Μόνο σε περιορισμένο βαθμό. Εάν η τρύπα που έχει ανοίξει είναι σημαντικά εκτός θέσης ή δεν είναι ευθεία, η συσκευή κοπής μπορεί να ακολουθήσει το υπάρχον σφάλμα. Βελτιώστε πρώτα τη διαδικασία διάτρησης ή διάτρησης. Τι προκαλεί τη φλυαρία κατά τη διάρκεια της επανάληψης; Η φλυαρία μπορεί να προκύψει από υπερβολικό περιθώριο, κακή ακαμψία, λανθασμένη ταχύτητα, μεγάλη προεξοχή του εργαλείου, ασταθή γεωμετρία πριν από την οπή ή κακή ευθυγράμμιση μεταξύ του άξονα και της οπής. Πρέπει να μειώσω την ταχύτητα ή να κάνω τροφοδοσία για να σταματήσω τη φλυαρία του ρομαντικού; Μερικές φορές η μείωση της ταχύτητας βοηθά, αλλά δεν είναι πάντα η πρώτη λύση. Ελέγξτε πρώτα τη διαρροή, το περιθώριο, την ακαμψία του συγκρατητήρα και την ποιότητα προ-οπής. Η τροφή που είναι πολύ χαμηλή μπορεί επίσης να προκαλέσει τρίψιμο. Ποιες πληροφορίες πρέπει να στείλω όταν ζητάω υποστήριξη για την αντιμετώπιση προβλημάτων του ρεαλιστή; Στείλτε το υλικό του τεμαχίου εργασίας, τη διάμετρο προ-οπής, τη διάμετρο και την ανοχή στόχου, το βάθος οπής, την κατάσταση διαμπερούς οπής ή τυφλής οπής, τη μέθοδο ψυκτικού, την τρέχουσα ταχύτητα/τροφοδοσία, την προεξοχή εργαλείου, τον τύπο συγκράτησης και φωτογραφίες της επιφάνειας της οπής ή της φθαρμένης οπής. Σύναψη Η φλυαρία του καρβιδίου, οι υπερμεγέθεις τρύπες και η μικρή διάρκεια ζωής του εργαλείου είναι συνήθως προβλήματα διαδικασίας, όχι μόνο προβλήματα εργαλείων. Η πιο αποτελεσματική ακολουθία αντιμετώπισης προβλημάτων είναι η μέτρηση της προ-οπής, ο έλεγχος της εκροής, η αναθεώρηση του επιτρεπόμενου εύρους, η επιθεώρηση σημαδιών επιφάνειας και η προσαρμογή των παραμέτρων μία μεταβλητή κάθε φορά. Εάν αντιμετωπίζετε ασταθή ανοχή οπών, σημάδια φλυαρίας ή σύντομη διάρκεια ζωής του μηχανήματος,Επικοινωνήστε με το Supalμε το υλικό του τεμαχίου εργασίας σας, την κατάσταση προ-οπής, την ανοχή στόχου, τις τρέχουσες παραμέτρους και τις φωτογραφίες αστοχίας. Το Supal μπορεί να σας βοηθήσει να αξιολογήσετε εάν η βασική αιτία είναι το επίδομα, η εξάντληση, το ψυκτικό υγρό, η γεωμετρία του μηχανισμού άπλωσης ή η συνολική σταθερότητα της διαδικασίας.

2026

09/29